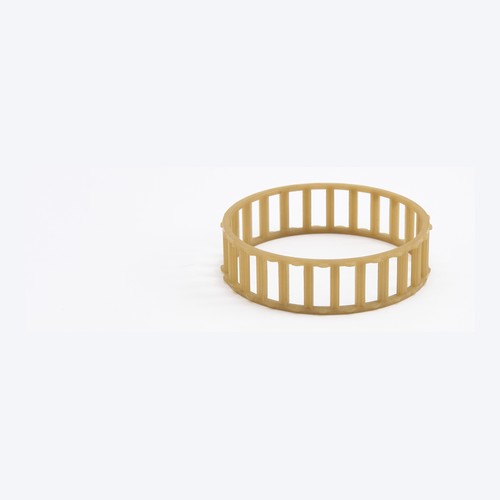
HF Series
One-way locking and overrunning
The cage pockets position and guide the locking rolling elements and associated spring elements in a one-way clutch.
Discuss your HF projectBearing structure
Plastic cages that position and guide rollers or locking elements in one-way clutch assemblies.
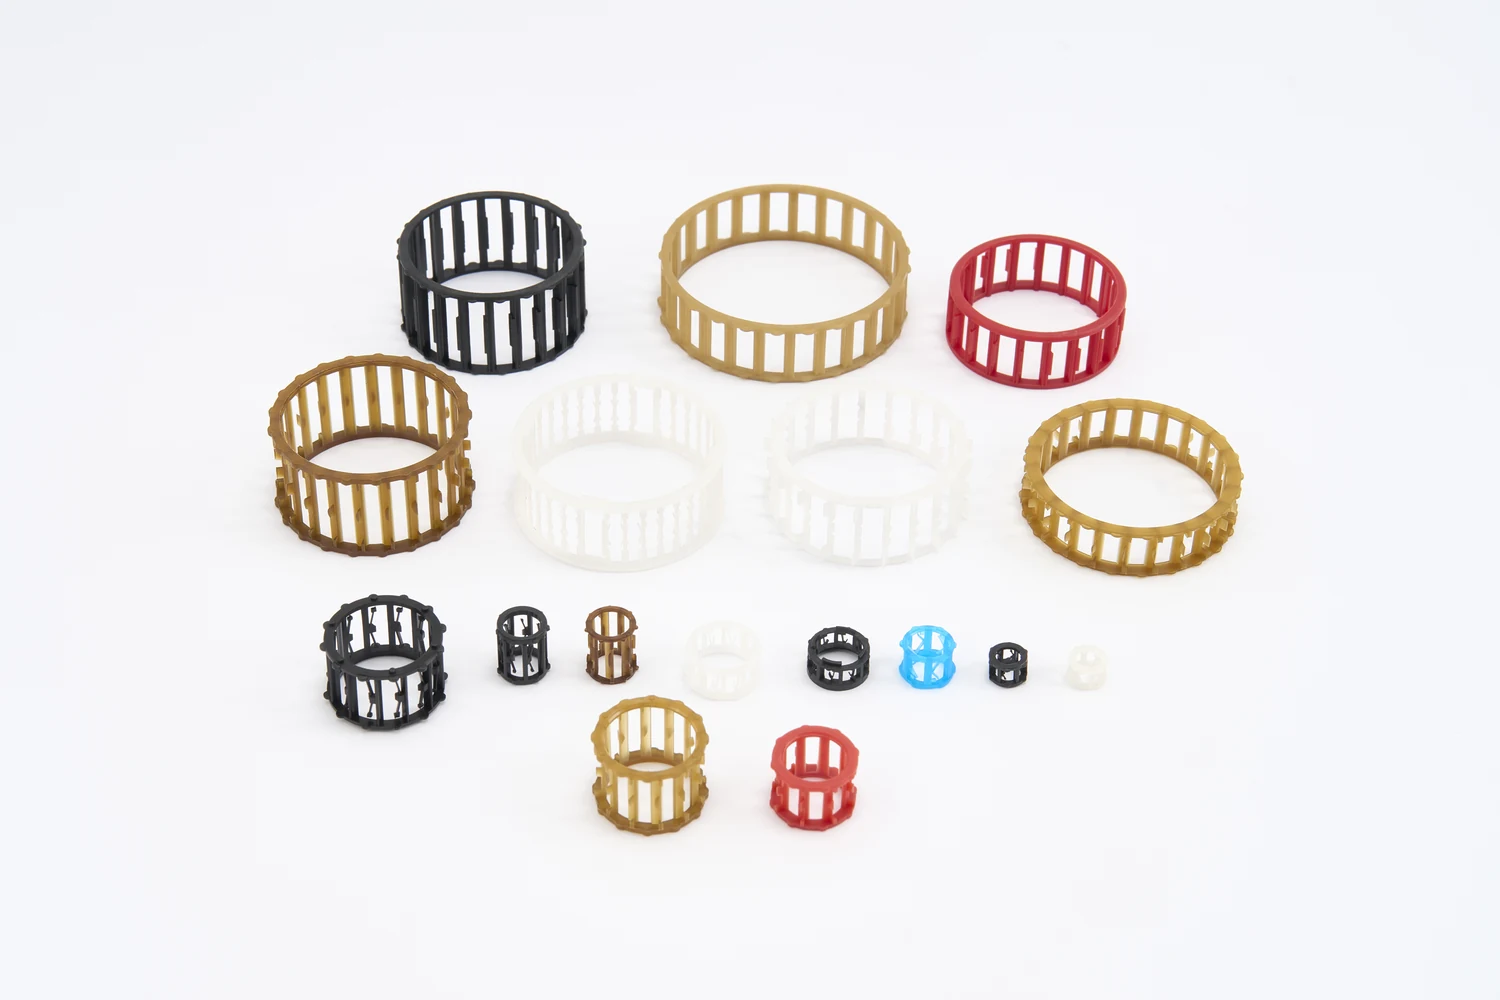
For overrunning, backstopping and indexing mechanisms. The cage geometry must match the locking elements, operating direction and surrounding assembly.
Supply scope: Plastic cages and plastic cage assemblies only. Rollers, springs, outer rings and complete one-way clutches are outside this supply scope.
One-way locking and overrunning
The cage pockets position and guide the locking rolling elements and associated spring elements in a one-way clutch.
Discuss your HF project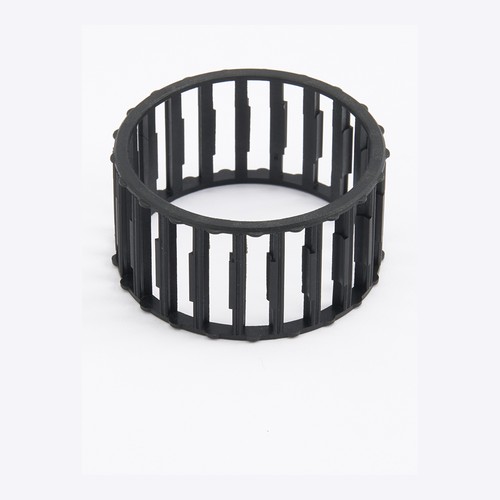
Three-piece design with bearing supports
The documented plastic cage arrangement has large-end, centre and small-end parts. The centre cage guides the locking elements; the end cages guide the supporting rolling elements.
Discuss your HFL projectThe polymer grade is selected for the project. Dimensional stability, cage flexibility, temperature and lubricant compatibility should be considered together.
Choose from the nylon materials below for your cage design and operating conditions. The specific resin grade is agreed for the project.
| Material code | Material description |
|---|---|
| PA66 | Unreinforced polyamide 66 |
| PA66-GF10 | 10% glass-fibre-reinforced polyamide 66 |
| PA66-GF15 | 15% glass-fibre-reinforced polyamide 66 |
| PA66-GF25 | 25% glass-fibre-reinforced polyamide 66 |
| PA66-GF30 | 30% glass-fibre-reinforced polyamide 66 |
| PA46 | Unreinforced polyamide 46 |
| PA46-GF15 | 15% glass-fibre-reinforced polyamide 46 |
| PA46-GF25 | 25% glass-fibre-reinforced polyamide 46 |
| PA46-GF30 | 30% glass-fibre-reinforced polyamide 46 |
| Property | PA66 | PA46 |
|---|---|---|
| Densityg/cm³ | 1.13–1.36 | 1.18–1.41 |
| Tensile stress, dryMPa | 85–190 | 100–210 |
| Tensile modulus, dryGPa | 3.0–10.0 | 3.3–10.0 |
| Melting point, DSC°C | ≈260 | ≈295 |
| Heat deflection temperature°C · 1.8 MPa | 75–250 | 190–290 |
Ranges summarise the example resin grades below for initial material selection. Finished-part performance is reviewed for the selected grade and application. Tensile stress uses dry yield or break values. Continuous operating temperature is assessed separately for the grade and conditions.
Boerjing develops molds and manufactures precision injection-molded plastic parts from customer drawings or approved samples. We support mold trials, sample approval, small-batch validation and repeat production.
Start with the component and intended use. Share available drawings or samples, material requirements and expected quantities.